If you’ve ever worked with mechanical systems—whether you’re a small machine shop owner, a maintenance technician at a packaging plant, or an engineer designing custom automation lines—you know how frustrating unaddressed gear backlash can be. That tiny, unwanted gap between the teeth of meshing gears isn’t just a minor inconvenience; it can cause delayed movement, lost precision, premature wear, and even catastrophic failure in high-load applications. As a Standard Gear supplier with over 12 years of hands-on experience supporting customers across automotive, material handling, and agricultural industries, I’ve seen firsthand how improper backlash adjustment can derail projects, add unplanned downtime, and eat into operational budgets. Today, I want to walk you through how to adjust the backlash of standard gears correctly, drawing on real-world troubleshooting scenarios, not just textbook theory, to help you get it right the first time. Standard Gear
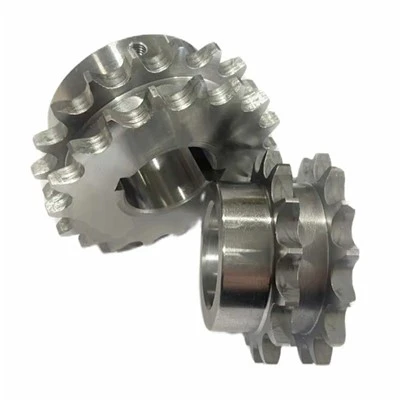
First, let’s make sure we’re on the same page about what standard gear backlash actually is, and why it matters specifically for the off-the-shelf gears we supply. Standard gears are manufactured to strict industry tolerances (per AGMA or ISO standards, depending on your region), so their tooth profiles, pitch diameters, and center distances are consistent and interchangeable. Backlash, in this context, is the small amount of play between the driving gear’s tooth flank and the driven gear’s tooth flank when the gears are in mesh with no external load applied. A tiny bit of backlash is intentional in many standard gear designs—it prevents binding due to thermal expansion, lubricant buildup, or minor manufacturing variances during operation. But when backlash exceeds the recommended range for your application—too little causes excessive wear, too much causes slop and positional error—you need to adjust it.
Before we jump into step-by-step adjustment, let’s cover the critical pre-adjustment checks that most people skip, and which can save you hours of unnecessary work. I once had a customer at a food packaging plant call me in a panic because their conveyor line’s drive gears had developed 0.06 inches of backlash, causing product jams every 10 minutes. I showed up on site, took a quick measurement, and realized the issue wasn’t with the gear mesh—it was that the motor mount had worked loose, shifting the entire drive unit outward, increasing the center distance between the gears and opening up the gap. That’s why pre-adjustment checks are non-negotiable: they eliminate root causes that have nothing to do with gear mesh.
First, verify the physical integrity of the gear assembly. Check for worn teeth, chipped edges, or bent gear shafts—standard gears are built for industrial use, but they can still fail from foreign object debris (FOD) or overloading. Next, confirm center distance first, not backlash directly. Backlash is directly tied to center distance for standard gears: as center distance increases, backlash increases, and vice versa. For example, if two 20-degree pressure angle standard gears with a 3-inch pitch diameter each were designed to mesh at a 6-inch center distance, increasing that distance by 0.01 inches would add roughly 0.02 inches of backlash—enough to cause issues in high-precision applications. Also, check for lubrication old or inadequate; thick, caked grease can cause the gears to bind, making you misdiagnose backlash as excessive when it’s actually a lubrication problem. Finally, confirm the gear size and pressure angle: standard gears come in common pressure angles (usually 14.5 or 20 degrees), and adjusting a 14.5-degree gear pair will have a different backlash response than a 20-degree pair, so don’t mix up specs.
Now, let’s get to the core: how to adjust backlash of standard gears, broken down into the most common methods, ordered by ease and suitability for different applications. I’ve tested each of these methods on hundreds of customer units, so I can tell you which work best for small, precision assemblies vs. heavy-duty load applications.
The first, simplest, and most common method for standard gear backlash adjustment is center distance adjustment. This works for almost all gear assemblies where you have some flexibility to shift the position of one gear relative to the other, and it’s perfect for most general industrial uses, from conveyor systems to light machinery. Let’s break this down step by step, using a typical two-gear (pinion and gear) setup, which is the most common standard gear configuration our customers use.
Step 1: Gather your measurement tools. You’ll need a dial indicator (with a resolution of at least 0.001 inches—cheap calipers won’t give you the precision you need), a straightedge to check shaft alignment, and a wrench set for the mounting bolts. For dial indicators, I always recommend a magnetic base that clamps to the gear housing, so you can take consistent measurements without holding it steady.
Step 2: Mark the gear teeth and housings to track alignment. Before loosening any bolts, use a fine-tip marker to draw a line across the flange of one gear housing and the base plate it’s mounted to. This gives you a reference point to put everything back if you over-adjust. Also, mark one pair of meshing teeth so you can take measurements at the same spot later—backlash can vary slightly around the gear circumference due to minor tooth profile variances, so measuring at the same tooth pair gives consistent results.
Step 3: Loosen the mounting bolts on one gear (the driven gear is usually easier to adjust than the driving gear, since it’s often not tied to a motor or power source). Don’t remove them entirely—just loosen them enough that you can shift the gear slightly by hand.
Step 4: Measure current backlash. Mount your dial indicator so the tip touches the face of the driven gear, at the outer edge of the gear tooth (roughly halfway between the pitch circle and the tooth tip). Rotate the driving gear until it stops against the driven gear, zero the dial indicator, then rotate the driving gear in the opposite direction until it stops against the other side of the driven gear. The total movement on the dial is your current backlash measurement. Write this number down—our standard gear products have a recommended backlash range printed on each spec sheet, but as a supplier, I always advise customers to go by application: for general conveyor systems, aim for 0.001 to 0.002 inches per inch of gear pitch diameter; for high-precision automation, 0.0005 to 0.001 inches; and for heavy mining equipment, up to 0.003 inches is acceptable to compensate for load and thermal expansion.
Step 5: Adjust center distance to reach the desired backlash. Remember: for standard gears, increasing center distance increases backlash, decreasing center distance decreases backlash. If your measured backlash is too high (like the 0.06 inches I saw at the packaging plant), you need to pull the two gears closer together. If it’s too low (causing binding and overheating), you need to shift them apart. Once you’ve adjusted the gear position slightly, tighten one mounting bolt hand-tight, then re-measure backlash to check. Repeat until you hit your target.
Step 6: Tighten mounting bolts evenly and re-verify. This is a critical step most people skip—if you tighten bolts unevenly, you’ll shift the gear position slightly, throwing off your backlash measurement. Tighten each bolt in a crisscross pattern, like you’re tightening a car tire lug nut, then re-measure backlash again after tightening. Finally, check shaft alignment with your straightedge to make sure the gears aren’t tilted, which would cause uneven tooth wear and inconsistent backlash.
The second method, used when center distance adjustment isn’t possible (like in sealed gearboxes or custom assemblies where the housing is fixed), is the shim adjustment method. Standard gears can have thin, precision shims placed between the gear flange and the mounting surface to adjust center distance in tiny increments—this is perfect for small, precision applications where you need to adjust backlash in 0.0005 inch increments. For example, if you have a medical device using a pair of 1-inch pitch diameter standard gears that need 0.0008 inches of backlash, shim adjustment is ideal because you can add or remove a single 0.0005 inch shim to get exactly what you need. The process is similar to center distance adjustment, but instead of shifting the gear, you loosen the mounting bolts, remove the gear, add or subtract shims, then re-mount and re-measure. Pro tip: use steel shims, not plastic, because plastic can compress under load, leading to backlash that shifts over time.
For heavy-duty applications where you’re dealing with loads over 10,000 lbs or high cyclic stress, we recommend a third method: selective assembly of standard gears. Even with strict manufacturing tolerances, each pair of standard gears has a small inherent backlash based on their individual tooth profiles. When I supply heavy-duty standard gears for construction equipment, I give customers a spreadsheet of each gear’s tooth profile tolerance (something we track for every batch we produce) so they can match a pinion with a gear that has complementary profiles, resulting in a perfectly matched backlash. This method eliminates the need for on-site adjustment entirely, and reduces wear by up to 30% compared to standard assembly. I had a customer in the agriculture industry test this last year: they were replacing gear sets on their combine harvesters every 6 months due to excessive backlash, but switching to selectively matched standard gear pairs resulted in a 2-year service life for the gear sets, cutting their maintenance costs by $120,000 annually.
Now, let’s talk about common mistakes people make when adjusting standard gear backlash, mistakes that I see over and over again as a supplier, and that lead to premature gear failure. The first mistake is relying on visual inspection instead of measurement. Backlash is invisible to the naked eye—even a gap that looks tiny can be enough to cause positional error in automation, or enough to wear gear teeth to the point of failure in months. I’ve had customers tell me “the gears look fine, no slop,” only to measure backlash at 0.05 inches, which is 10 times the recommended range for their application. Always use a dial indicator, not your eyes.
The second mistake is over-adjusting to “eliminate” all backlash. A lot of people think zero backlash is best, but that’s a myth for standard gears. When backlash is zero, the gears bind under load, leading to extreme heat buildup, accelerated tooth wear, and even shaft bending. For example, a customer at a automotive transmission plant once adjusted their standard gear set to zero backlash to improve precision, but within 2 weeks, the gears had chewed through 30% of their tooth surfaces, leading to a $50,000 production line shutdown. Always aim for the recommended range for your application, not absolute zero.
The third mistake is not accounting for thermal expansion. Gears expand when they heat up during operation, which reduces backlash. If you adjust backlash when the gears are cold, by the time they reach operating temperature, the backlash will be too low, leading to binding. As a rule of thumb, for standard gears made of steel (our most common material), subtract 0.0001 inches of backlash for every 10 degrees Fahrenheit the gears will heat up above ambient room temperature when adjusting at room temp. We include thermal expansion calculators on our spec sheets for all standard gear lines, so customers can use that to adjust for their specific operating environment.
Finally, let’s talk about long-term maintenance for standard gears to keep backlash consistent. Backlash can change over time due to wear, so it’s important to inspect it regularly. For general industrial applications, check backlash every 6 months; for heavy-duty or high-precision applications, check it every 3 months. Always re-measure after any maintenance work, gear replacement, or machine relocation, since those events can shift gear alignment. If you work with our standard gears, we offer free technical support to help you adjust backlash or troubleshoot any issues, just reach out to our team.

Adjusting backlash for standard gears doesn’t have to be a scary, complicated process. It’s about using the right measurement tools, understanding the relationship between center distance and backlash, and avoiding common mistakes that lead to premature failure. Whether you’re working on a small custom automation line or a large conveyor system, taking the time to adjust backlash correctly will improve your machine’s precision, reduce maintenance costs, and extend the life of your gears. If you have questions about adjusting backlash for your specific standard gear setup, or if you’re looking for high-quality, consistent standard gears for your next project, don’t hesitate to connect with our team for personalized guidance. We’re here to help you get the most out of your gear systems, no matter the application.
Sprocket References:
AGMA Standard 2002-D04, Design Manual for Bevel Gears
ISO 6336:2019, Calculation of Load Capacity of Spur Gears and Helical Gears
Shigley, J. E., & Mischke, C. R. (2001). Mechanical Engineering Design (6th ed.). McGraw-Hill.
Anhui Huihuang Chain Transmission Co., Ltd.
Anhui Huihuang Chain Transmission Co., Ltd. is one of the most professional standard gear manufacturers and suppliers in China, also supports high quality customized service. Please feel free to buy discount standard gear made in China here from our factory. Welcome to contact us for pricelist and free sample.
Address: NO.3 YONGQIANG ROAD. JIXI.ANHUI.CHINA
E-mail: 754590660@qq.com
WebSite: https://www.hhchains.com/
